Meta description: Learn how ISO 5 (Class 100) and ISO 7 (Class 10,000) cleanrooms affect optical bonding yield, and how Golden Margins combines an ISO 5 core with WACKER silicone-based FLOCA technology for industrial displays.
Why Cleanliness Is a Core Process Condition
Traditional air-gap assembly leaves an air layer between the display module and the cover glass. This causes refractive index mismatch, light scattering, internal condensation, and dust ingress, all of which reduce contrast and outdoor readability.
Optical bonding removes the air gap by laminating the layers together with a liquid optical adhesive. It also introduces a new challenge: because the adhesive flows and the glass is highly sensitive, a single particle of 0.5 μm or larger trapped at the interface can create a visible speck, dark spot, or bubble nucleus. A cleanroom is therefore not a supporting facility. It is a process condition that directly determines yield, defect rate, and long-term reliability.
ISO 5 vs. ISO 7: Key Differences
| Parameter | ISO 5 (Class 100) | ISO 7 (Class 10,000) |
|---|---|---|
| Max. particles ≥0.5 μm | ≤3,520 per m³ | ≤352,000 per m³ |
| Airflow pattern | Unidirectional (laminar) | Non-unidirectional (turbulent) |
| Air changes per hour | 240–600 | 30–60 |
| FFU ceiling coverage | 60%–80% | 15%–25% |
| Construction & operating cost | Very high | Moderate |
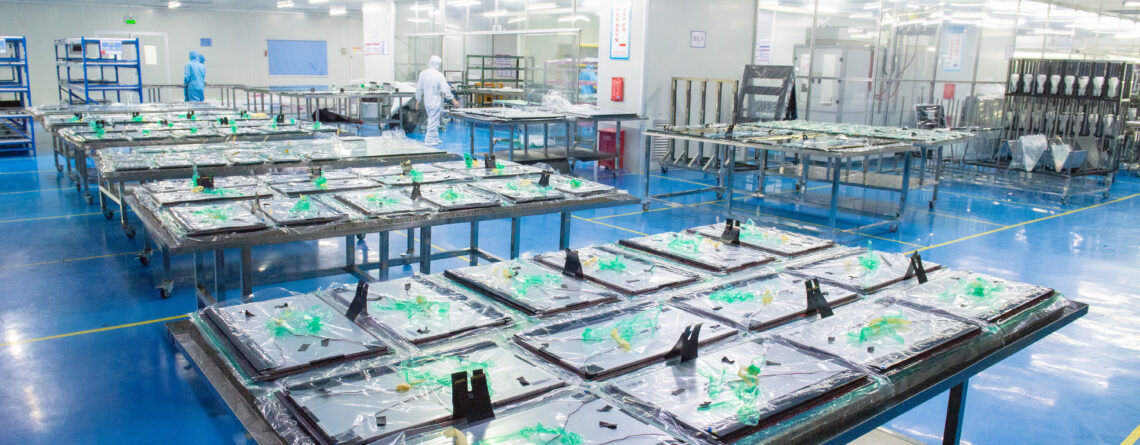
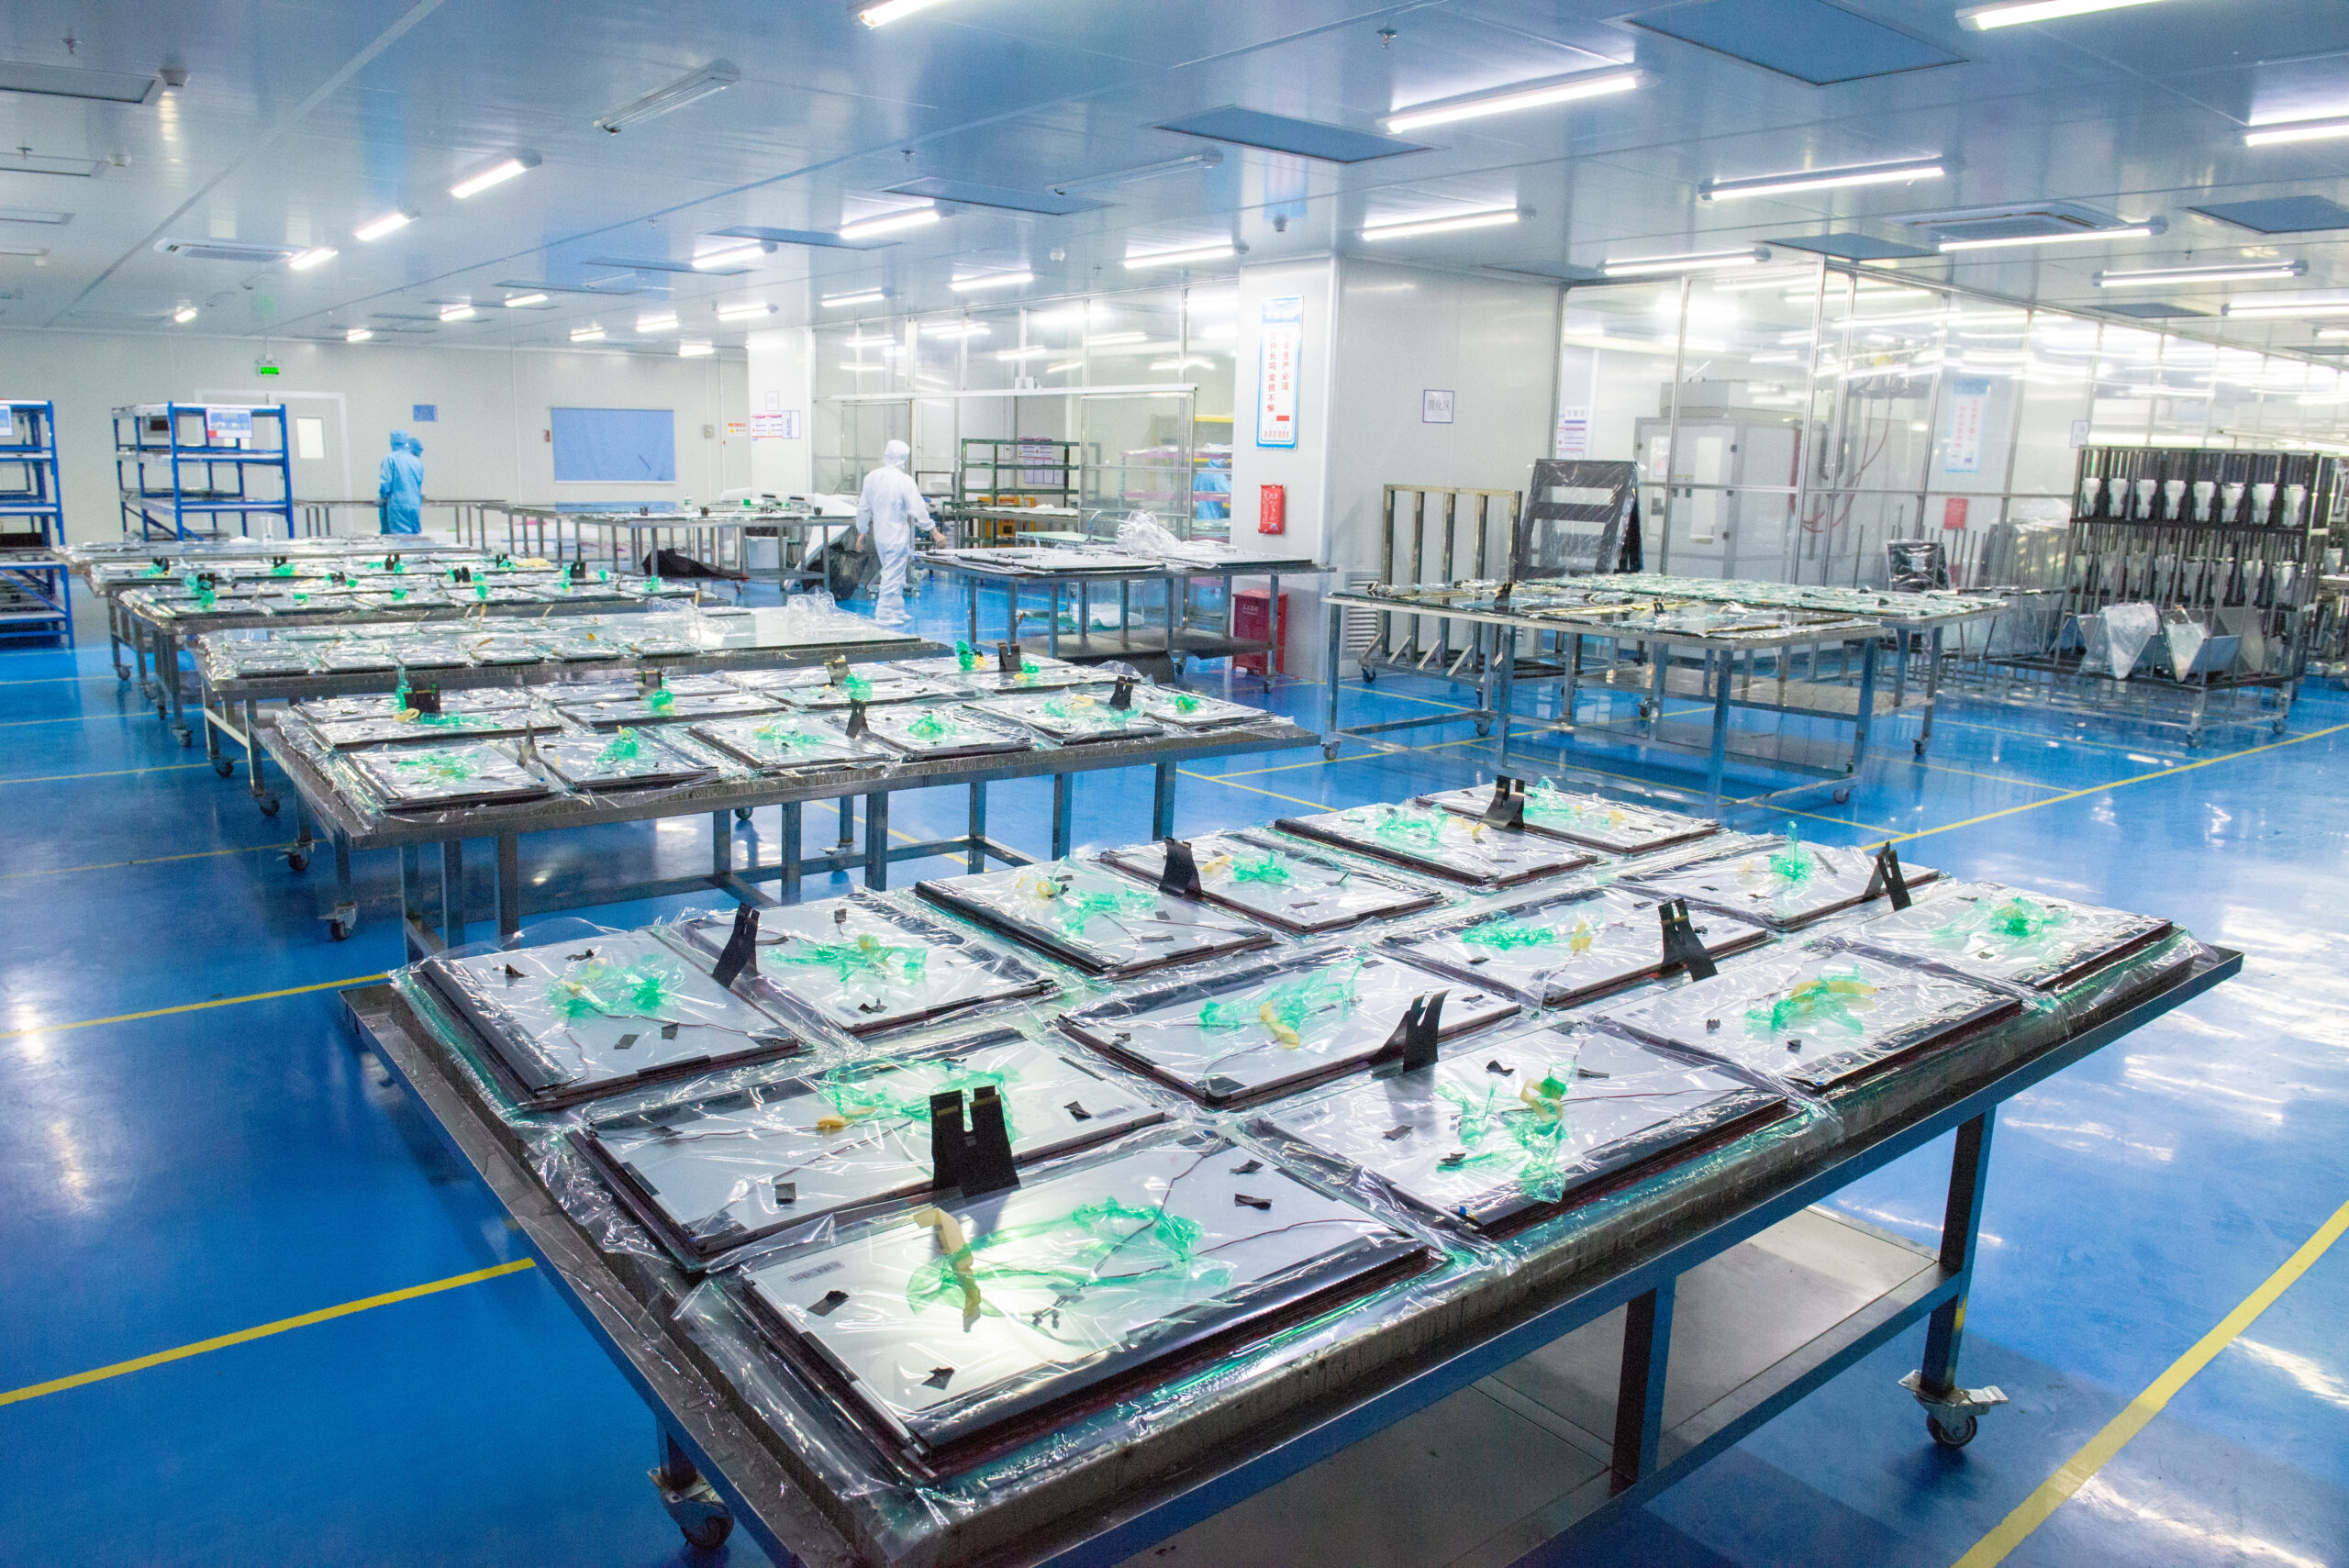
An ISO 5 environment holds particle concentration to roughly 1% of an ISO 7 room. Vertical laminar airflow at approximately 0.3–0.5 m/s pushes particles downward in a piston-like pattern, so exposed glass and uncured adhesive stay free of settling contaminants.
The Cleanliness Cascade
Because ISO 5 space is costly to build and run, well-designed facilities allocate it by process sensitivity:
- ISO 5 core zone: the steps most sensitive to particles, including incoming inspection, alignment, adhesive filling, and pre-cure handling.
- ISO 7 support zone: less sensitive or already-sealed operations, including unpacking, housing pre-assembly, secondary edge sealing, final assembly, logistics, and gowning transition.
This structure delivers zero-tolerance for foreign matter where it matters, without sacrificing throughput or cost efficiency.
Our Approach: FLOCA Technology in an ISO 5 Environment
Golden Margins operates a 3,800 m² smart manufacturing facility with monthly capacity exceeding 200,000 units. Every optical bonding step is performed in an ISO 5 cleanroom under ISO 9001:2015 and IATF 16949 quality systems, following an eight-step process:
- Dual incoming inspection of TP and LCM
- LCM UV frame sealing
- Precision alignment and cavity preparation
- Pressure-free WACKER silicone injection
- Thermal chamber curing at 50–60 °C
- Precision cleaning and microscopic inspection
- Secondary edge sealing
- 100% final QC and 10-point capacitive touch calibration
Our proprietary FLOCA (Full-Lamination Optical Clear Adhesive) process uses industrial-grade silicone from WACKER, Germany, which provides:
- Yellowing resistance: The Si–O backbone (bond energy up to 445 kJ/mol) remains optically clear under prolonged heat and intense sunlight.
- Low stress: Volumetric shrinkage below 1.0% prevents polarizer distortion, edge light leakage, and moiré patterns.
- Wide-temperature resilience: The cured, flexible elastomer absorbs shock and vibration from −20 °C to +70 °C and helps prevent internal condensation and fogging.
This controlled process enables bonding yields of 92%–95% on large-format modules such as 43-inch 4K displays, supported by 100% inspection from IQC to OQC, with no sampling.
How We Compare
| Dimension | Standard Industrial Panel PCs | Tier-1 Industrial Brands | Golden Margins |
|---|---|---|---|
| Bonding method | Mainly air-gap or frame bonding | OCA/LOCA; high cost at large sizes | FLOCA full lamination as standard |
| Cleanroom class | ISO 7 or general workshop | High-standard cleanroom | ISO 5 core zone |
| Operating temperature | 0–50 °C | 0–50 °C (some wide-temp models) | −20 to +70 °C |
| Inspection | AQL sampling | Key-process sampling plus final QC | 100% inspection, zero sampling |
| Customization & lead time | Fixed standard models | 8–12 weeks | Flexible OEM/ODM, short lead time |
What This Means for Your Project
For system integrators, self-service kiosk makers, medical device manufacturers, and industrial automation teams, display selection is a decision about life-cycle reliability and total cost of ownership. Our design priorities reflect that:
- Optics and touch: ≥98% light transmittance, zero parallax, excellent sunlight readability, touch response ≤3 ms, and accuracy within ±0.5 mm.
- Thermal and structural design: CNC-machined anodized aluminum frames (thermal conductivity approx. 160–220 W/m·K) act as a passive heat sink for fanless operation, eliminating fan failures caused by dust and oil. IP65 front-panel protection.
- Integration: Built-in dual-lens camera, passport/ID reader, QR code scanner, and array microphone reduce exposed cabling and on-site maintenance.
- Value and flexibility: High yield lowers material waste, keeping large-format optical bonding competitively priced. We support custom I/O, AG/AR/AF coatings, and structural modifications without compromising IP65 or optical specifications.
Conclusion
Cleanliness sets the ceiling for optical bonding quality. ISO 5 zones protect the most critical steps, while ISO 7 zones support efficient flow and assembly. Combined with WACKER silicone, FLOCA technology, and 100% inspection, this system lets Golden Margins deliver industrial displays that stay clear, stable, and reliable in demanding environments.